Let Us Know How We Can Help. We Are Your Dedicated Solutions Provider.
Choosing China Top Pp Non Woven Fabric Manufacturers requires more than scanning export lists. The market includes spunbond, meltblown, laminated, and recycled options. Each serves different uses, from shopping bags to medical packaging. Pp Non Woven Fabric can look similar on a sample roll. Performance may differ under tension, heat, moisture, and repeated folding.
Experienced buyers inspect GSM, roll width, color consistency, and sealing behavior. They also ask how suppliers control raw materials and production changes. A reliable manufacturer should provide clear specifications. Batch records matter. Independent testing can confirm tensile strength, elongation, and hygiene-related requirements where applicable. Factory visits, video audits, and sample approvals add practical evidence. Still, no single certificate proves every claim.
This guide introduces leading Chinese suppliers through a buyer-focused lens. It considers manufacturing history, equipment, export experience, and communication quality. It also examines whether a factory can support stable volume without sacrificing consistency. Details such as clean winding, firm cores, clear labels, and protected pallets reveal daily discipline. Pricing receives attention, but the lowest quotation may hide thinner material or weaker packaging. That risk deserves careful calculation.
Readers should compare like-for-like specifications before requesting final offers. Questions about lead times, minimum order quantities, customization, and after-sales support remain essential. Some rankings may change as capacity, certifications, and market conditions change. That limitation should be stated openly. The strongest choice is not always the largest factory. It is the supplier whose evidence matches your application. With documented checks and realistic trials, buyers can narrow the field responsibly.
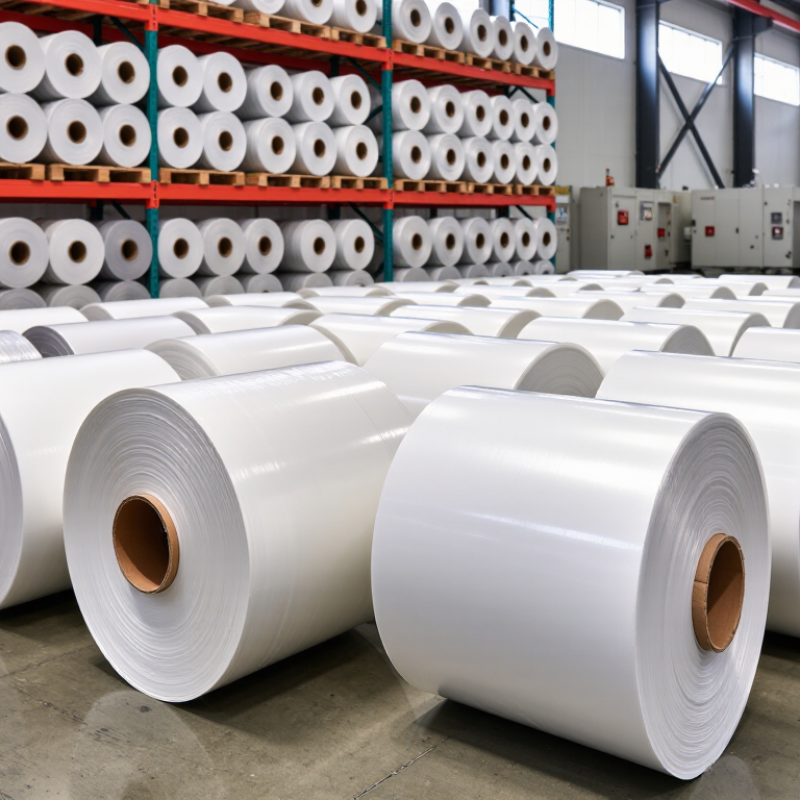
PP nonwoven fabric is a web of polypropylene fibers bonded without traditional weaving. Manufacturers form the fibers through spunbond, meltblown, or thermal bonding processes. The result is a lightweight, breathable, and water-resistant sheet. It may feel like paper, but its structure is closer to a controlled fiber network.
According to Smithers’ The Future of Global Nonwovens to 2028, the worldwide nonwovens market was worth over US$50 billion in 2023. Polypropylene remains important because it offers low density, chemical resistance, and efficient processing.
In production, fabric weight is usually measured in GSM, or grams per square meter. A 20 GSM sheet feels light, while a 100 GSM sheet provides stronger support. However, GSM alone does not prove quality. Fiber diameter, bonding strength, pore size, and uniformity also matter. This is where some product descriptions become too simple.
Tips: Ask for GSM and tensile test results. Check samples in both dry and wet conditions. For disposable applications, confirm whether the fabric is designed for single use. Also question vague claims such as “fully recyclable,” because recycling depends on contamination, collection systems, and local facilities. Quality testing should follow recognized methods, such as ISO or ASTM procedures.
In China, PP non woven fabric usually begins with polypropylene pellets, color masterbatch, and carefully measured additives. Workers feed these materials into an extruder, where heat melts the polymer into a smooth, flowing material. Temperature control matters. Too much heat can weaken the fibers, while uneven heating may create unstable output.
The molten polymer passes through a spinneret with hundreds of tiny holes. Air stretches the streams into continuous filaments, which land on a moving screen and form a loose web. The web then receives bonding treatment. Thermal bonding uses heated rollers, while spunbond lines may combine stretching and cooling in one continuous process. Needled or laminated structures require different equipment and inspection standards.
Experienced factories check fabric weight, thickness, tensile strength, elongation, color, and air permeability. Operators often test samples from the roll edges and center because results may differ. A practical mistake can happen here: focusing only on laboratory figures may overlook rough edges or inconsistent winding. That is why production teams inspect both machine data and the physical roll.
Manufacturers adjust die temperature, line speed, airflow, and roller pressure for bags, hygiene products, filtration layers, agriculture covers, and packaging. Every application needs a different balance. Cheaper output is not always better. Reliable production depends on traceable materials, calibrated instruments, trained operators, and honest records of defects.
| Manufacturing or Evaluation Dimension | Typical Data or Industry Range | How It Is Applied in China | Quality-Control Point |
|---|---|---|---|
| Primary polymer | Polypropylene resin, usually supplied as pellets; spunbond grades commonly have a melt flow rate of approximately 25–40 g/10 min, while meltblown grades are generally much higher. | Manufacturers select polymer grade according to fiber fineness, fabric strength, filtration performance, and end use. | Incoming-resin checks normally include melt flow rate, moisture, contamination, color, and lot traceability. |
| Pellet feeding and extrusion | PP is melted in an extruder at temperatures typically around 200–240°C, depending on resin grade and line design. | Automated gravimetric feeders and continuous extrusion systems are widely used for stable output and consistent basis weight. | Operators monitor melt temperature, pressure, throughput, screen condition, and residence-time stability. |
| Fiber-forming method | The two principal PP technologies are spunbond and meltblown. Spunbond produces continuous filaments; meltblown produces very fine short microfibers. | Spunbond is used for bags, hygiene products, agriculture, and medical textiles. Meltblown is used mainly for filtration and absorbent or composite structures. | Fiber diameter, filament uniformity, die cleanliness, and web appearance are inspected during production. |
| Typical fiber fineness | Spunbond fibers are commonly in the approximate range of 1.5–3.5 denier. Meltblown fibers are much finer and are often measured in micrometers rather than denier. | The selected fineness affects softness, tensile strength, filtration efficiency, breathability, and surface uniformity. | Microscopic examination and finished-fabric performance testing are used to verify fiber distribution. |
| Web formation | Extruded fibers are cooled, stretched, and deposited on a moving forming belt to create a web. Airflow and belt speed control web uniformity. | Production lines are configured for single-layer, dual-layer, or multi-layer structures such as spunbond–meltblown–spunbond composites. | Cross-direction basis-weight variation, visible defects, holes, streaks, and fiber clumps are checked. |
| Bonding process | Thermal calendering is common for spunbond fabrics. Bonding conditions are adjusted according to PP melting behavior, fabric weight, and embossing pattern. | Point-bond patterns are frequently used to balance tensile strength, softness, drape, and air permeability. | Bond strength, thermal damage, hole formation, embossing clarity, and fabric hand feel are evaluated. |
| Common basis-weight range | Spunbond PP fabrics are commonly produced from approximately 10–150 g/m². Meltblown layers are often lighter, depending on filtration and composite requirements. | Low weights are used for hygiene and lightweight packaging; medium and heavy weights are used for bags, furniture, construction, and agriculture. | Basis weight is measured by cutting and weighing specimens in accordance with ISO 9073-1 or an equivalent method. |
| Fabric width and roll format | Commercial production widths commonly range from approximately 1.6 to 3.2 meters, with custom widths available depending on the production line. | Finished rolls may be supplied in jumbo rolls or slit rolls for converting into bags, medical products, packaging, and technical textiles. | Roll width, roll length, winding tension, telescoping, edge alignment, and splice control are recorded. |
| Color and functional additives | Common options include white, black, colored, UV-stabilized, hydrophilic, hydrophobic, antistatic, and flame-retardant grades. | Additives may be introduced through masterbatch, surface treatment, or a combination of both, depending on the intended application. | Color difference, additive dispersion, surface wettability, UV performance, and regulatory compliance are tested where applicable. |
| Core performance tests | Typical tests include tensile strength, elongation, tear resistance, air permeability, hydrostatic pressure, thickness, basis weight, and dimensional stability. | Testing frequency may be set by the buyer’s specification, production lot, application risk, and applicable national or international standard. | Common reference methods include ISO 9073-1 for mass per unit area, ISO 9073-3 for tensile strength, and ISO 9237 for air permeability. |
| Factory qualification criteria | Relevant criteria include production-line width, annual capacity, process stability, laboratory capability, traceability, export experience, and documented quality procedures. | A qualified supplier should provide technical data sheets, samples, inspection records, material declarations, and a clear method for handling nonconforming rolls. | Buyers should verify actual production samples rather than relying only on catalog specifications or stated capacity. |
| Packing and shipment inspection | Rolls are generally protected with moisture-resistant outer packaging and labeled with product code, lot number, width, basis weight, and production date. | Export shipments are prepared according to container loading limits, roll dimensions, destination regulations, and buyer-specific packaging requirements. | Final inspection should confirm quantity, roll identification, packaging integrity, appearance, and consistency with the approved sample. |
Note: The values shown are typical industry ranges and process references. Exact specifications vary by PP grade, equipment configuration, fabric structure, end use, and customer requirements.
When evaluating Chinese PP non woven fabric manufacturers, begin with measurable production standards, not attractive photos. Confirm whether the factory produces spunbond, meltblown, or composite fabric in-house. Ask for recent test reports showing basis weight, thickness, tensile strength, tear resistance, and air permeability. Each result should match the requested width and color. Small differences matter. A 10% GSM variation can affect sewing, filtration, or packaging performance. Request samples from normal production, not only carefully selected pieces. This reveals consistency across rolls.
Reliable suppliers can explain resin sources, additive control, batch coding, and storage conditions. Their quality system should include incoming inspection, online monitoring, and final roll checks. Verify applicable ISO, GB, ASTM, or EN testing methods with an independent laboratory when the order is important. Factory audits should examine calibration records, worker training, defect handling, and traceability. Do not treat one certificate as proof of total quality. It is only one signal. Review production capacity, lead times, minimum order quantities, and backup plans in writing. A low quotation may hide unstable supply or weak inspection. That is where judgment is needed.
Tips: Compare at least three sample batches. Rub the surface, measure GSM, and inspect winding edges under bright light. Record every result in a simple supplier scorecard. No checklist is perfect. Recheck performance after washing, heat exposure, or converting, because laboratory results may not reflect your process. Ask direct questions, document unclear answers, and keep approval samples sealed for future comparison.
Leading PP Non Woven Fabric Manufacturers in China
China’s leading PP non woven fabric manufacturers serve hygiene, medical, agriculture, packaging, and construction markets. Their core materials include spunbond, meltblown, SMS, and laminated structures. Production quality depends on polymer purity, web uniformity, line speed, and storage control.
Grand View Research reported that the global nonwoven fabrics market reached about USD 53.51 billion in 2022. It also forecast a 7.2% compound annual growth rate from 2023 to 2030. This demand encourages Chinese manufacturers to improve automation and export consistency. However, capacity alone proves little. Buyers should inspect GSM tolerance, tensile strength, elongation, air permeability, and roll-to-roll variation. I would not treat a glossy sample as proof. Laboratory results matter more.
Tips: Request recent test reports, production photos, and a small trial order. Confirm whether the quoted GSM includes coating or lamination. Ask for batch records and packaging details. The cheapest quotation can look efficient. It often is not. Also verify compliance with the destination market’s textile and product-safety requirements through independent testing. China’s strong supply chain can shorten lead times, but communication errors still occur. A clear specification sheet should define width, color, core size, packing method, and acceptable defects before production.
Representative basis-weight specifications commonly used in China’s PP spunbond nonwoven industry. Higher basis weights are generally selected for stronger, more durable applications, while lighter grades are used for hygiene and disposable products. The figures are application references rather than company or brand rankings.
Selecting a Chinese PP non woven fabric supplier requires more than comparing export prices. Ask how long the factory has produced PP spunbond fabric, and request dated production records. A capable team should explain GSM, width, roll length, elongation, and tensile strength without vague answers. Ask for evidence.
Request samples from different production batches, not one carefully chosen roll. Check surface uniformity, edge cutting, odor, winding tension, and color consistency under strong light.
Measure the fabric yourself when possible. A small GSM difference can affect sewing, filtration, packaging, or agricultural performance. It happens.
Supplier audits should include
Confirm whether polypropylene sources are traceable and whether inspection records match your purchase specifications. Ask for relevant test reports, production capacity, lead times, and corrective-action procedures. A low quotation may hide unstable quality or weak after-sales support.
Clear communication matters during sampling and mass production.
Record every requirement in a signed technical sheet, including tolerance limits and packaging details. Evaluate how the supplier handles an unexpected defect.
A reliable partner reports problems early and proposes measurable solutions. No checklist is perfect.
Recheck critical dimensions before shipment, because trust should support inspection, not replace it.